


About Helium Mining
ASIC mining hardware manufacturer serving commercial mining operations worldwide.
Who We Are
Founded in 2017, Helium Mining develops ASIC mining systems for commercial and private mining operations. Today, the company is headquartered in China, with regional logistics offices, test labs, and support teams across Singapore, North America, and Central Asia.
Our mining machines operate in commercial data centers and private mining farms across more than 30 countries. We build air-cooled, hydro-cooled, and immersion-compatible mining rigs designed to run reliably around the clock using grid power or renewable energy sources.
From the Beginning to Today
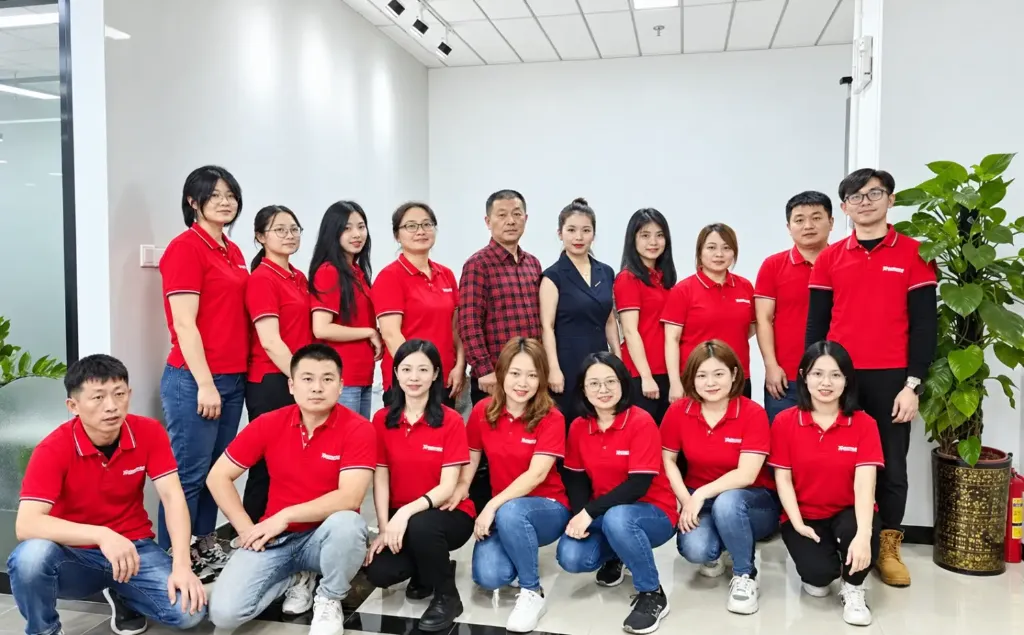
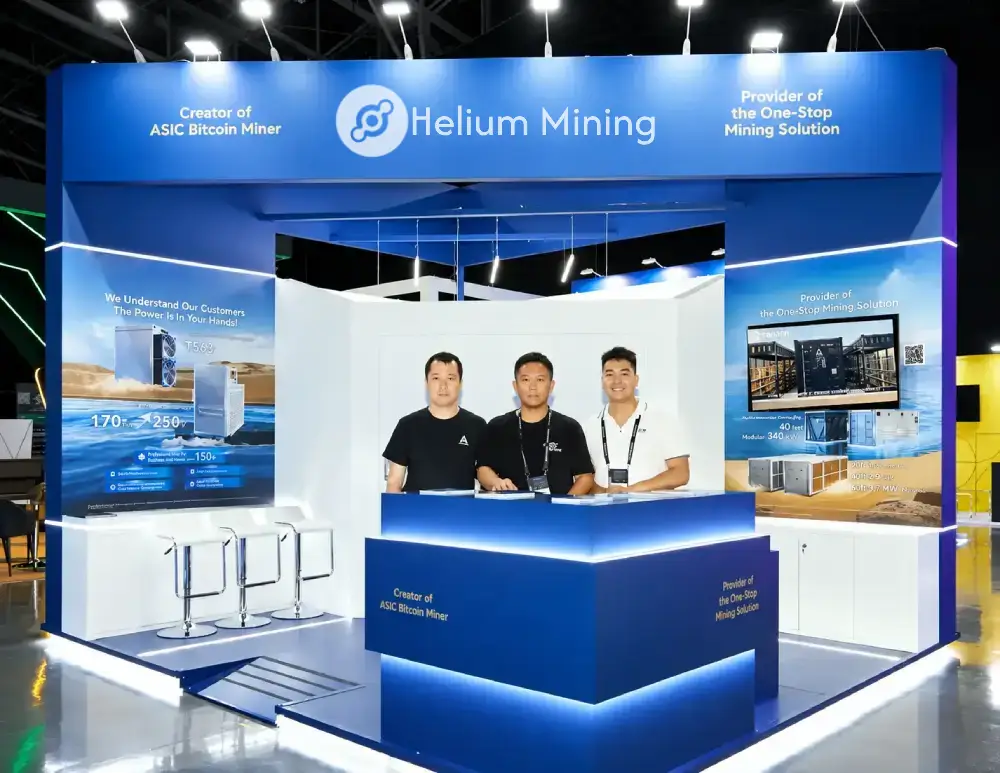
Helium Mining was founded in 2017 with a focus on Bitcoin mining hardware, later expanding into ASIC systems for other mining algorithms and cryptocurrencies. In the early days of Bitcoin, miners had to use desktop graphics cards (GPUs) and programmable chips (FPGAs). Our team built the first commercial ASIC miner, demonstrating that custom-designed silicon could deliver higher performance while using far less electricity.
Since then, our manufacturing has expanded from small-scale laboratory assembly to automated cleanroom production. We handle the key production steps ourselves: multi-layer circuit board layout, automated component placement, heatsink mounting, power-supply assembly, and control firmware development.
Every miner that leaves our factory is built for continuous operation in data center conditions, with full serial-number tracking and factory warranty support.
How We Build
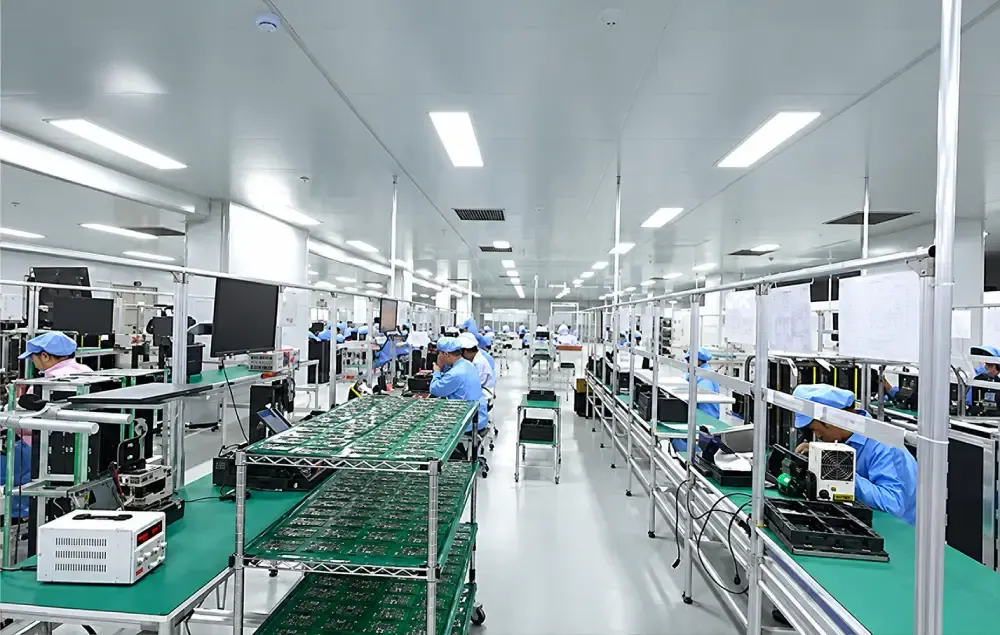
Circuit Board Assembly (SMT)
Automated pick-and-place machines position chips and components on custom multi-layer circuit boards. Boards then pass through reflow ovens and automated optical inspection (AOI) to verify solder joint quality.
Chassis Assembly & Cooling
Hashboards are installed in aluminum chassis with extruded heatsinks. Thermal compound is applied, and the heatsink fasteners are tightened to the specified torque. Hydro models undergo liquid-channel pressure testing to guarantee leak-free operation.
24 to 48-Hour Full-Load Burn-In Testing
Every assembled miner runs for 24 to 48 consecutive hours under full load in climate-controlled test bays. Technicians monitor hashrate stability, board temperatures, and voltage regulation to catch any component defects before shipping.
Serial Numbering & Packaging
Each unit receives a unique serial number linked to its burn-in test results and official 365-day limited warranty. After a final visual check, the miner is fitted with tamper-evident security seals and packed into shock-absorbing cartons.
How We Work
Three principles guide how we design hardware, test machines, and work with clients:
Direct Supply Without Middlemen
We supply hardware directly to commercial hosting farms and private mining operators alike, with transparent factory pricing and no forced distributor markups.
Bench-Tested Specifications
Every specification in our product sheets comes from real bench measurements. Hashrates, power draw, and operating temperatures are recorded under full load in standard ambient conditions.
Power Efficiency & Longevity
Electricity is the primary cost in mining. We design power supplies for high conversion efficiency, build durable cooling systems, and develop firmware that protects the chips during long-term operation.
What We Build
Our product catalog covers hardware systems for commercial mining sites:
Air-Cooled ASIC Miners
Standard form-factor rigs built with custom ASIC chips. Key features include automatic board-level voltage tuning, variable-speed fan cooling, and built-in hardware health monitoring.
- Custom ASIC chips designed for Bitcoin mining
- Automated board-level voltage and frequency regulation
- Built-in web dashboard for status checks and setup
Hydro & Liquid Cooling Models
Miners built for closed water loops and immersion cooling tanks. Liquid cooling removes noisy fans, lowers auxiliary power consumption, and protects hashboards from dust and humidity.
- Compatible with dielectric oil tanks and water manifolds
- Factory-sealed CNC cooling plates
- Heat-recovery support for building or facility heating
Matched Power Supply Units
Server-grade power supplies built specifically for the power draw of our hashboards, delivering high electrical conversion efficiency and stable DC output to reduce electrical stress on components.
- High-efficiency AC-to-DC power conversion
- Over-voltage, short-circuit, and thermal trip protection
- Digitally signed firmware to prevent unauthorized code
Energy and Cooling
Power efficiency and temperature management are important during continuous mining operations. Many commercial facilities are located near hydroelectric dams, wind farms, and solar farms where electricity is cleanest and most affordable.
Standards and Certifications
Our equipment complies with international safety and electromagnetic standards for commercial computing environments.
European Conformity
Meets European Union safety and electromagnetic compatibility requirements for commercial computing machinery.
Electromagnetic Compatibility
Tested under commercial and industrial digital device limits to minimize radio-frequency interference.
Restricted Substances
Manufactured without prohibited concentrations of lead, mercury, cadmium, and other hazardous substances.
Quality Management
Covers assembly procedures, parts inspection, and documented testing records across manufacturing locations.
View Products and Specifications
Browse our current catalog of air-cooled and hydro-cooled mining systems.